Oct 8, 2026 · NEWS
A bin body with a 2.2mm wall and a 3.0mm base will always pull differently as it cools. We adjust cavity dimensions after mould-flow simulation so the finished part — not the steel — matches the drawing.
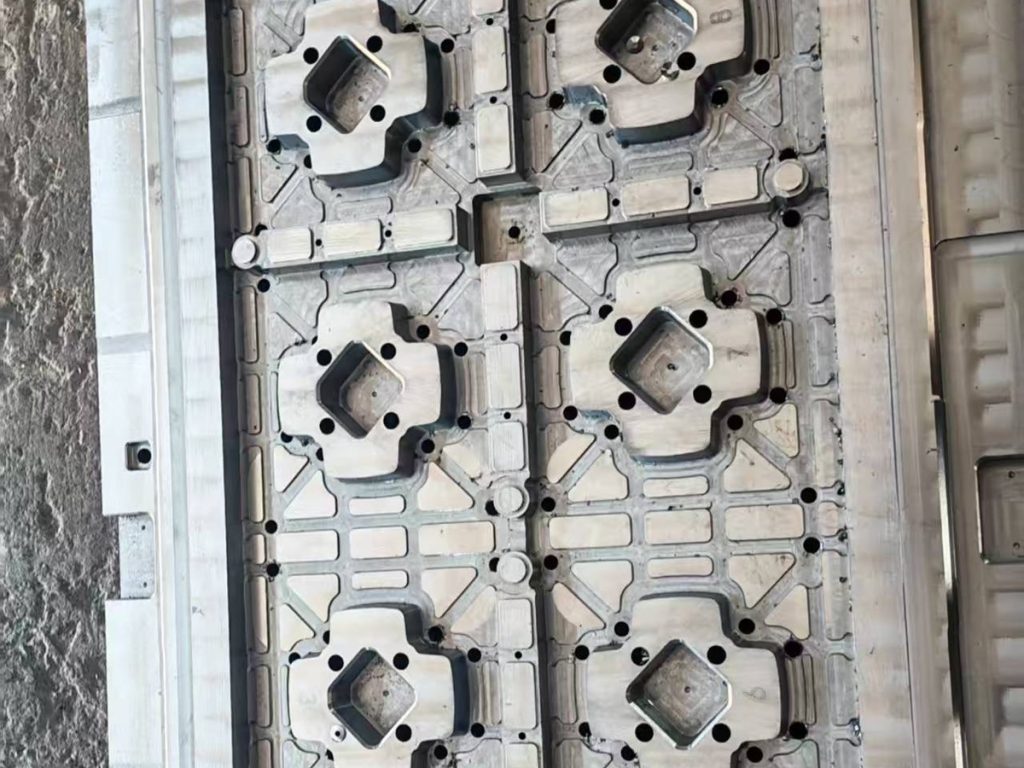
Baffles and bubblers are placed in the core so the inner and outer walls cool at a similar rate. An unbalanced core is the most common reason a bin leans to one side after ejection.
Draft angles and ejector placement are checked against the actual part stiffness. Too few ejectors, or ejectors on a thin wall, will leave a permanent bow that no amount of packing pressure can fix.